Air Humidification for Terminal Comfort at Nuremberg Airport
In-room humidification

ML Princess spray head

High pressure spray heads for larger facilities

The ML Princess has a unique and patented design ensuring the right amount of ultrafine water particles being evaporated into the air using high pressure technology. The design ensures no dripping from the high pressure nozzles and the fan inside ensures the right speed and flow. The ML Princess is ideal to use in larger production facilities with high ceilings.

High volume spray head for large-scale humidification

The Condair ML Princess is a high-pressure humidification system designed to maintain stable humidity levels in production facilities and industrial environments.

Equipped with an integrated fan and up to eight high-pressure nozzles, the system distributes a fine mist throughout the surrounding air, supporting efficient and consistent humidification.

The ML Princess is available in two versions: ML Princess 2, with a humidification capacity of 10–36 L/h, and ML Princess 2 Max, with a capacity of 52 L/h.

With adjustable fan speed and a choice of nozzle sizes, the system can be configured to meet different humidification requirements and installation conditions.

Hygienic by design

The ML system typically operates with reverse osmosis (RO) treated water to ensure high water quality and reliable humidification. For applications requiring even higher water purity, additional water treatment options, are available.

An integrated distribution fan helps disperse the fine water mist evenly throughout the surrounding air, promoting efficient evaporation and consistent humidity control. This supports stable indoor climate conditions across the humidified area.

Recommended application

The ML Princess spray heads are well suited for humidification and evaporative cooling in manufacturing and production environments across a wide range of industries. Designed for high-capacity performance, they provide reliable humidity control in facilities with varying operational demands. The system is suitable for installations with ceiling heights from as low as 3.6 metres, making ML Princess a flexible solution for production areas where space limitations must be considered without compromising humidification efficiency.
Humidification directly in the room with high-pressure humidifiers
thumbnail

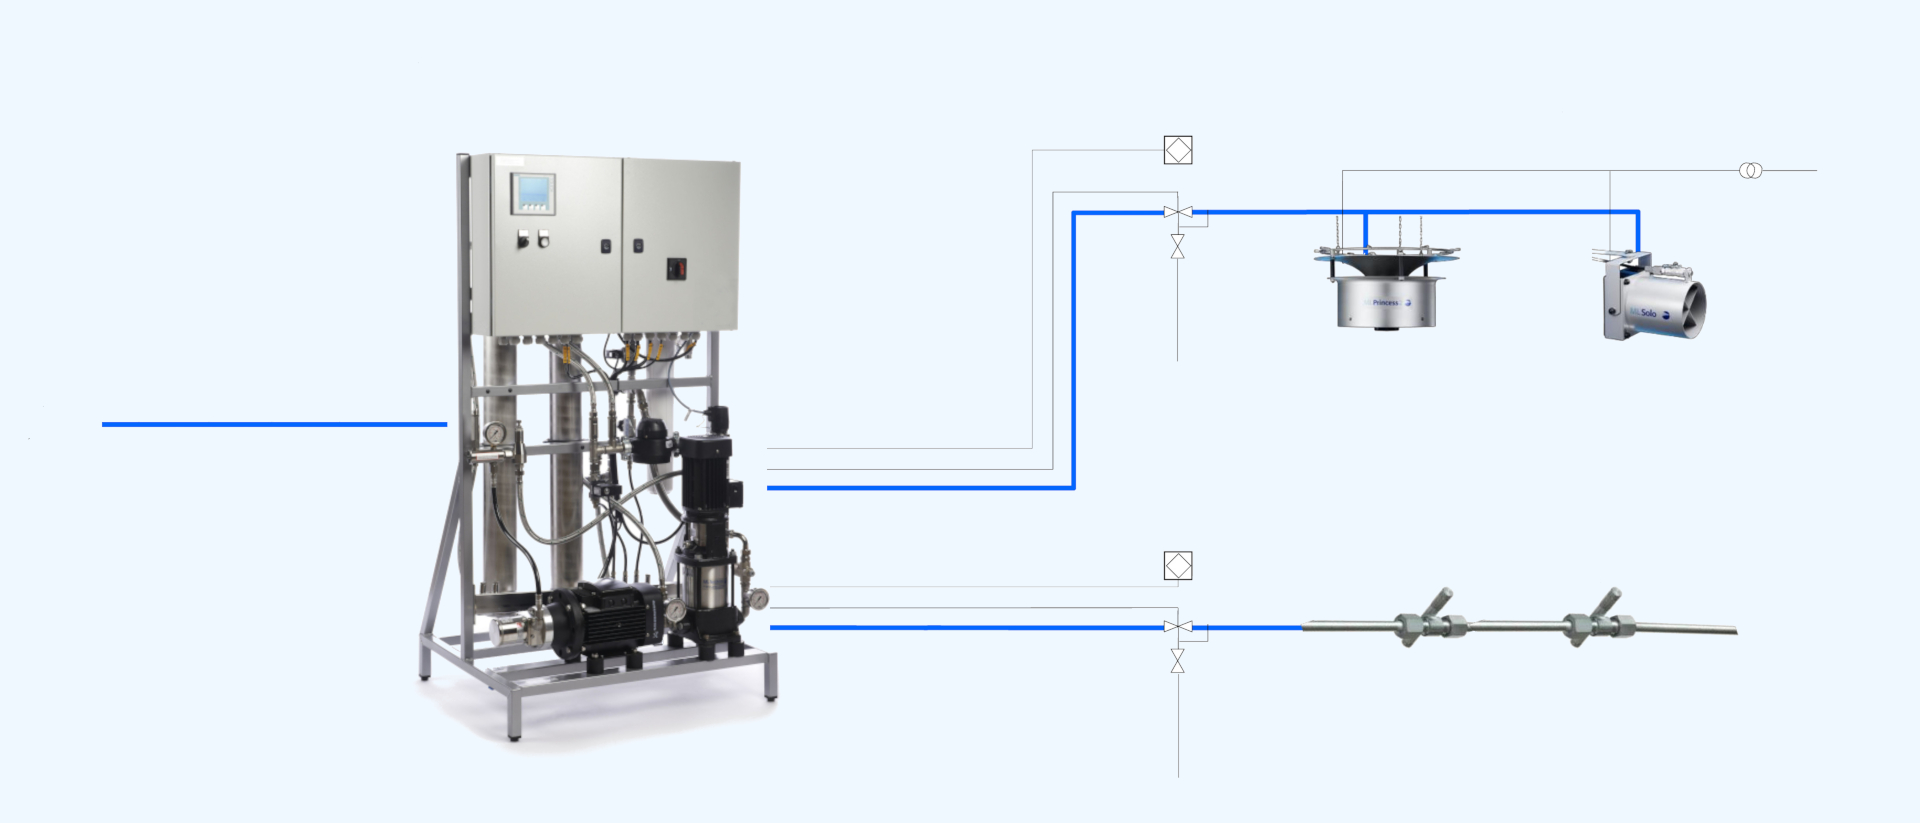
High-pressure humidifiers

High-pressure humidifiers atomise water into microfine aerosols with very low energy consumption. The humidifiers can provide individual humidity control for different zones.

Solenoid valve

Controls the water flow to the direct room humidifiers, regulated by local sensors in the zones and rooms to be humidified.

Sensors

Local sensors that measure and regulate stable relative humidity in individual zones (e.g. rooms and work areas).

Water treatment

Water inlet with pre-treatment (filter stages and softening) to protect against limescale deposits, organic contaminants, dirt and sand particles.

MLP RO

Reverse osmosis and high-pressure pump are combined in a single space-saving installation. The modules are assembled in various sizes depending on the humidification capacity.

Solenoid valve

Controls the water flow to the direct room humidifiers, regulated by local sensors in the zones and rooms to be humidified.

Sensors

Local sensors that measure and regulate stable relative humidity in individual zones (e.g. rooms and work areas).

High-pressure humidifiers

High-pressure humidifiers atomise water into microfine aerosols with very low energy consumption. The humidifiers can provide individual humidity control for different zones.

High-pressure humidifiers

High-pressure humidifiers atomise water into microfine aerosols with very low energy consumption. The humidifiers can provide individual humidity control for different zones.

High-pressure humidifiers

High-pressure humidifiers atomise water into microfine aerosols with very low energy consumption. The humidifiers can provide individual humidity control for different zones.
Other spray heads in the ML series

Discover Condair in action

Service and know-how

WERNER KENKEL Sp. z o.o., Krzycko Wielkie (Poland)

For packaging manufacturer Werner Kenkel, controlled humidity has a direct impact on production and quality assurance. More speed, consistent quality and less waste are the most important advantages.

Bart Sp. z o.o, Świecie (Poland)

The packaging specialist Bart Sp. z o.o not only ensures the quality of its products with modern direct room air humidification, but also lowers the temperature and dust generation in production at the same time.

Nordan, Wolsztyn (Poland)

Protected wood through optimal humidity The NorDan Group is one of the leading manufacturers of wooden windows and doors. High-pressure air humidification ensures quality at all stages of production at the Group's Wolsztyn site. The Polish site in Wolsztyn has been one of the NorDan Group's largest production facilities since 2006: over 200 members of staff produce 10.000 wooden windows there for Scandinavia and the United Kingdom each year. Stable processes and production conditions are enormously important for us. It is therefore essential to have constant, optimal humidity, explains the chief engineer, Maciej Sosiński.

Preston Sp. z o.o., Poznan (Poland)

A constant relative humidity of 50 per cent ensures that Preston Packaging’s printing process runs smoothly, without any material distortion, and with a high degree of registration accuracy during the subsequent die-cutting and gluing stages.

Fritz Hansen, Rawicz (Poland)

The international design brand Republic of Fritz Hansen is famous for exclusive design classics such as the EggTM lounge chair or the 7TM chair series. With innovative craftsmanship and premium quality, the Danish company, founded in 1872, sets standards worldwide.

Ashley Furniture Industries (Wi)

Ashley Furniture Industries, Inc. is the largest manufacturer of furniture in the world. Established in 1945, Ashley offers one of the industry's broadest product assortments to retail partners in 123 countries.

Batesville Casket Company

Batesville Casket Company is a manufacturer of caskets and cremation urns. The company is a subsidiary of Hillenbrand, Inc., and is headquartered in Batesville, Indiana.

Quaker Oats

The Quaker Oats Company is an American food conglomerate based in Chicago. It has been owned by PepsiCo since 2001.

Allegro Coffee

HMF Group

HMF Group improved paint quality and reduced production costs with a Condair ML high-pressure humidification system. By maintaining a constant 45% RH in the paint shop, the solution virtually eliminated paint defects, reduced energy consumption by up to 50% during winter and delivered a payback period of less than one year.

Jydsk Aluminium Industri

Jydsk Aluminium Industri installed a Condair adiabatic cooling system to maintain a stable production temperature of 22°C while significantly reducing energy consumption. The solution reduced electricity used for cooling from approximately 350,000 kWh to less than 25,000 kWh per year, while improving employee comfort and ensuring consistent production quality.

TERMA

Terma saves 150,000 kWh annually Terma is an international manufacturer of high-tech equipment for customers within the aviation, defence, space and monitoring system industries. Condair's humidification solution provides free evaporative cooling while offering Terma considerable energy savings. Broad product range meets strict requirements Terma requires excellent air quality and accurate humidity control in its production areas, which e.g.involves protection against electrostatic discharge that may potentially interfere with processes and damage electronic components. Energy savings through evaporative coolingAnother focus area for Terma is the company's energy consumption. Terma has opted for a humidification solution with evaporative cooling for direct room humidification - the absolutely least expensive alternative compared with other humidification systems. Wherever possible in the production areas, Terma is gradually switching to Condair's evaporative cooling and humidification solutions, which has contributed to considerable energy savings. In less urgent areas, or where previously chosen ventilation solutions exist, Terma continues to use Condair's steam humidifiers, which represent the appropriate solution for these particular purposes. Advantages Saves more than 150,000 kWh annually Reduces electrostatic discharges (ESD) Utilises free evaporative cooling Ensures compliance with product tolerances Increases employee well-being System specifications Pumps: MLP 300 with RO Modules: 7 x Princess 2 Capacity: 250 l/h Installed: 2013 "An energy seminar at Condair opened our eyes to new opportunities of reducing our energy consumption through evaporative cooling. At the same time, our indoor climate is now considerably better, which of course is popular with the employees." Terma Facilities, Gert Jorgensen

Calibre Inc.

Calibre Inc. is an Employee Owned Company operating multiple facilities within Southeastern Wisconsin since 1981. They provide painted part solutions for use in exclusive Powersports products.

AVEC American Veneer Edgebanding

American Veneer Edgebanding Company, Inc.,USA (A.V.E.C.),was established in Heath, Ohio, in 1997. A.V.E.C. distributes veneer edgebanding products especially to the North American wood working industry. Their modern, humidity controlled warehouse facility is conveniently located close the Columbus International Airport.

Siemens - Wind Turbines

Quotes from our customers

WERNER KENKEL Sp. z o.o., Krzycko Wielkie (Poland)Piotr WojciechowskiTechnical Director

"Our experience shows that we can produce faster and with less waste due to the optimal humidity. This reduces costs and makes our processes more efficient."
Nordan SP. z o.o., Wolsztyn (Poland)Maciej SosińskiSenior Engineer

"Stable processes and production conditions are extremely important to us. That is why consistent, optimal humidity is also essential."
Fritz Hansen, Rawicz (Poland)Maciej WaldmajerMaintenance Manager

"Air humidification is an integral part of our quality management, on which we have to rely 100%."
Preston Sp. z o.o., Poznan (Poland)Filip KarońskiCEO

"Thanks to air humidification, we no longer have problems with electrostatics, which in the past often led to production interruptions."
Air Humidification for Terminal Comfort at Nuremberg Airport

Information package: In-room humidification

Always the right fit – find out more here!

In-room humidifiers are used specifically where humidity is required. Suitable for every application and room size, ideal for retrofitting, energy-efficient and easy to maintain.

Request your free information package here and get a free thermo-hygrometer to measure your humidity!

Contact us

We look forward to hearing from you and discussing your requirements for in-room humidification for your application.

Click here for further information or a personal consultation.

Need more information or have a question?

Contact us via our contact form for in-room solutions

Contact a Condair consultant directly

Find the right Condair contact persons in your region for in-room solutions